


Page 640 - Yamawa_European_Catalogue_YEU21
P. 640
3. Flutes

    Intro


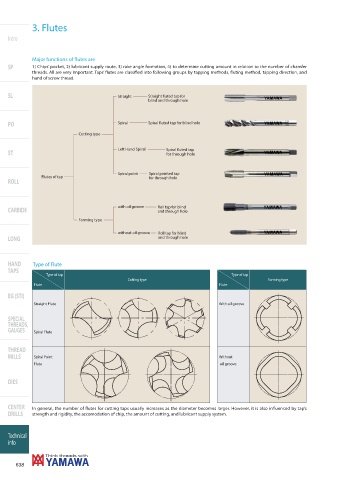
            Major functions of flutes are
    SP      1) Chips’ pocket, 2) lubricant supply route, 3) rake angle formation, 4) to determine cutting amount in relation to the number of chamfer
            threads. All are very important. Taps’ fl utes are classifi ed into following groups by tapping methods, fl uting method, tapping direction, and
            hand of screw thread.

    SL                                    Straight   Straight fluted tap for
                                                     blind and through hole


    PO                                    Spiral
                             Cutting type

                                          Left Hand Spiral
    ST


                                          Spiral point  Spiral pointed tap
                Flutes of tap                        for through hole
    ROLL


                                          with oil groove  Roll tap for blind
    CARBIDE                                             and through hole
                             Forming type

                                          without oil groove  Roll tap for blind
    LONG                                                 and through hole


    HAND     Type of Flute
    TAPS
                 Type of tap                                                      Type of tap
                                              Cutting type                                     Forming type
             Flute                                                            Flute
    EG (STI)
             Straight Flute                                                   With oil groove

    SPECIAL
    THREADS,
    GAUGES   Spiral Flute


    THREAD
    MILLS    Spiral Point                                                     Without
             Flute                                                             oil groove

    DIES


    CENTER  In general, the number of fl utes for cutting taps usually increases as the diameter becomes larger. However, it is also infl uenced by tap’s
    DRILLS  strength and rigidity, the accomodation of chip, the amount of cutting, and lubricant supply system.


    Technical
    info


       638

