


Page 630 - Yamawa_European_Catalogue_YEU21
P. 630
Center Drills


              AUPEQ
    Intro


    SP
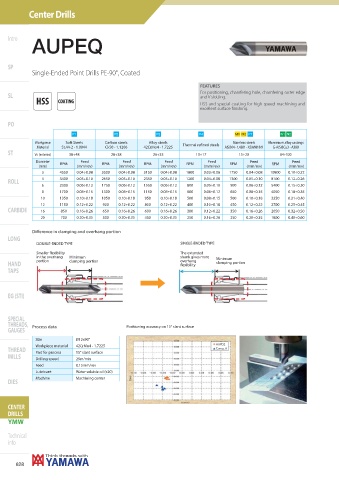
              Single-Ended Point Drills PE-90°, Coated

                                                                       FEATURES
                                                                         For positioning, chamfering hole, chamfering outer edge
    SL                                                                 and V slotting.
              HSS    COATING                                             HSS and special coating for high speed machining and
                                                                       excellent surface fi nishing.

    PO
                              P1             P2             P3             P4         M1   M2   P7      N1   N2


             Workpiece  Soft Steels   Carbon steels  Alloy steels  Thermal refi ned steels  Stainless steels  Aluminium alloy castings
              Material  St.44-2 - 1.0044  Ck50 - 1.1206  42CrMo4 - 1.7225       AISI304 - 1.4301 - X5XrNi18-9  G-AISi8Cu3 - A380
    ST       Vc (m/min)  38÷48          28÷38          26÷33          13÷17          13÷20         84÷120
              Diameter  RPM  Feed    RPM    Feed    RPM    Feed   RPM     Feed    RPM    Feed   RPM     Feed
               (mm)         (mm/rev)       (mm/rev)       (mm/rev)       (mm/rev)       (mm/rev)      (mm/rev)
                3     4550  0.04÷0.08  3500  0.04÷0.08  3150  0.04÷0.08  1800  0.03÷0.06  1750  0.04÷0.08  10800  0.10÷0.22
                4     3400  0.05÷0.10  2650  0.05÷0.10  2350  0.05÷0.10  1200  0.04÷0.08  1300  0.05÷0.10  8100  0.12÷0.26
    ROLL
                6     2300  0.06÷0.12  1750  0.06÷0.12  1550  0.06÷0.12  800  0.05÷0.10  900  0.06÷0.12  5400  0.15÷0.30
                8     1700  0.08÷0.15  1300  0.08÷0.15  1150  0.08÷0.15  600  0.06÷0.12  650  0.08÷0.15  4050  0.18÷0.35
                                                                                                        YMW-AUPEQ
               10     1350  0.10÷0.18  1050  0.10÷0.18  950  0.10÷0.18  500  0.08÷0.15  500  0.10÷0.18  3250  0.21÷0.40
               12     1150  0.12÷0.22  900  0.12÷0.22  800  0.12÷0.22  400  0.10÷0.18  450  0.12÷0.22  2700  0.25÷0.45
    CARBIDE    16     850   0.16÷0.26  650  0.16÷0.26  600  0.16÷0.26  300  0.12÷0.22  350  0.16÷0.26  2050  0.32÷0.50
               20     700   0.20÷0.35  500  0.20÷0.35  450  0.20÷0.35  250  0.16÷0.26  250  0.20÷0.35  1800  0.40÷0.60

            Diff erence in clamping and overhang portion
    LONG
              DOUBLE-ENDED TYPE                                 SINGLE-ENDED TYPE
              Smaller fl exibility                              The extended
              in the overhang   Minimum                         shank gives more   Minimum
              portion    clamping portion                       overhang
    HAND                                                        fl exibility  clamping portion
    TAPS


    EG (STI)


    SPECIAL
    THREADS,  Process data                   Positioning accuracy on 15° slant surface
    GAUGES
              Size          Ø12x90°
              Workpiece material  42CrMo4 - 1.7225                           AUPEQ
    THREAD                                                                   Comp. A
              Part for process  15° slant surface
    MILLS
              Drilling speed  25m/min
              Feed          0.15mm/rev
              Lubricant     Water soluble oil (x20)
              Machine       Machining center
    DIES


    CENTER
    DRILLS
    YMW

    Technical
    info


       628

