


Page 628 - Yamawa_European_Catalogue_YEU21
P. 628
Center Drills


              NC-SD V
    Intro


    SP
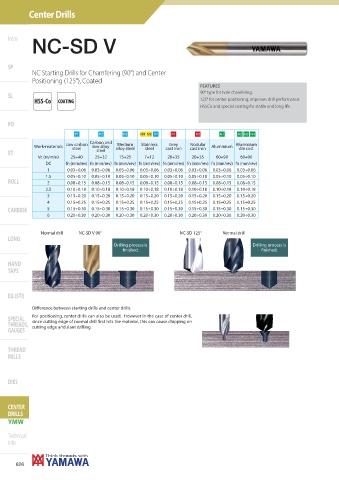
              NC Starting Drills for Chamfering (90°) and Center
            Positioning (125°), Coated
                                                                       FEATURES
                                                                         90° type for hole chamfering.
    SL
             HSS-Co  COATING                                             125° for center positioning, improves drill performance.
                                                                         HSSCo and special coating for stable and long life.


    PO
                               P1       P2      P3    M1   M2   P7      K1      K2      N1      N2   N3   N4


                        Low carbon   Carbon and   Medium   Stainless   Grey  Nodular  Aluminium
             Work-materials  steel  low alloy   alloy steel  steel  cast iron  cast iron  Aluminium  die cast
    ST                             steel
              Vc (m/min)  25÷40   25÷32    15÷25    7÷12    20÷35   20÷35    60÷90   60÷90
                 DC     fn (mm/rev) fn (mm/rev) fn (mm/rev) fn (mm/rev) fn (mm/rev) fn (mm/rev) fn (mm/rev) fn (mm/rev)
                  1      0.03÷0.06  0.03÷0.06  0.03÷0.06  0.03÷0.06  0.03÷0.06  0.03÷0.06  0.03÷0.06  0.03÷0.06
                 1.5     0.05÷0.10  0.05÷0.10  0.05÷0.10  0.05÷0.10  0.05÷0.10  0.05÷0.10  0.05÷0.10  0.05÷0.10
    ROLL          2      0.08÷0.15  0.08÷0.15  0.08÷0.15  0.08÷0.15  0.08÷0.15  0.08÷0.15  0.08÷0.15  0.08÷0.15
                 2.5     0.10÷0.18  0.10÷0.18  0.10÷0.18  0.10÷0.18  0.10÷0.18  0.10÷0.18  0.10÷0.18  0.10÷0.18
                                                                                                        YMW-NC-SD V
                  3      0.15÷0.20  0.15÷0.20  0.15÷0.20  0.15÷0.20  0.15÷0.20  0.15÷0.20  0.15÷0.20  0.15÷0.20
                  4      0.15÷0.25  0.15÷0.25  0.15÷0.25  0.15÷0.25  0.15÷0.25  0.15÷0.25  0.15÷0.25  0.15÷0.25
    CARBIDE       5      0.15÷0.30  0.15÷0.30  0.15÷0.30  0.15÷0.30  0.15÷0.30  0.15÷0.30  0.15÷0.30  0.15÷0.30
                  6      0.20÷0.30  0.20÷0.30  0.20÷0.30  0.20÷0.30  0.20÷0.30  0.20÷0.30  0.20÷0.30  0.20÷0.30


               Normal drill  NC-SD V 90°                        NC-SD 125°     Normal drill
    LONG
                                         Drilling process is                              Drilling process is
                                            fi nished.                                       fi nished.

    HAND
    TAPS


    EG (STI)

            Diff erence between starting drills and center drills
            For positioning, center drills can also be used.  However in the case of center drill,
    SPECIAL  since cutting edge of normal drill fi rst hits the material, this can cause chipping on
    THREADS,  cutting edge and slant drilling.
    GAUGES


    THREAD
    MILLS


    DIES


    CENTER
    DRILLS
    YMW

    Technical
    info


       626

