


Page 406 - Yamawa_European_Catalogue_YEU21
P. 406
Carbide Taps


              EH-CT
    Intro


             MS   Material Specifi c Series
    SP        Carbide Taps for Hard Materials (<55HRC), Coated


                                                                       FEATURES
                                                                         Carbide taps for high hardness steel (45 ÷ 55HRC).
    SL        HF     COATING                            5P               Specifi c design, ultra fi ne micrograin, suitable coating for
             CARBIDE          SYNCHRO                  THCHT           long and stable tool life.


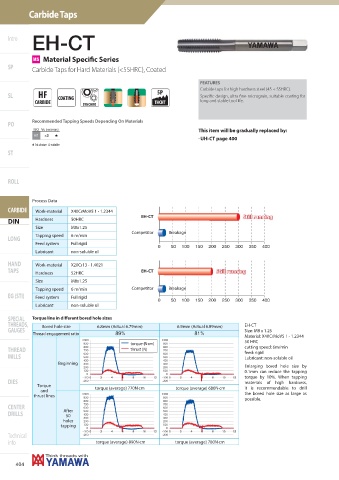
            Recommended Tapping Speeds Depending On Materials
    PO
               ISO   Vc (m/min)                                        This item will be gradually replaced by:
                 H1      ≤5       H
                                                                       . UH-CT page 400
            H 1st choice  I suitable
    ST


    ROLL

                                                                                                        DIN-EH-CT
            Process Data
    CARBIDE  Work-material  X40CrMoV5 1 - 1.2344
                                                                                      Still running
                                                   EH-CT                              Still running
    DIN      Hardness     50HRC
             Size         M8x1.25
                                               Competitor   Breakage
             Tapping speed  6 m/min
    LONG
             Feed system  Full rigid
             Lubricant    non-soluble oil
    HAND     Work-material  X20Cr13 - 1.4021
    TAPS     Hardness     52HRC                    EH-CT                     Still running
                                                                             Still running
             Size         M8x1.25
             Tapping speed  6 m/min            Competitor   Breakage
    EG (STI)  Feed system  Full rigid
             Lubricant    non-soluble oil

    SPECIAL  Torque line in diff erent bored hole sizes
    THREADS,    Bored hole size    6.8mm (Actual 6.79mm)       6.9mm (Actual 6.89mm)   EH-CT
    GAUGES                                                                             Size: M8 x 1.25
             Thread engagement ratio
                                                                                       Material: X40CrMoV5 1 - 1.2344
                                                                                       50 HRC
                                               torque (N·cm)
                                                                                       cutting speed: 6m/min
    THREAD                                     thrust (N)                              feed: rigid
    MILLS                                                                              Lubricant: non-soluble oil
                     Beginning
                                                                                       Enlarging bored hole size by
                                                                                       0.1mm can reduce the tapping
                                                                                       torque by 10%.  When tapping
    DIES                                                                               materials of high hardness,
              Torque              torque (average) 770N·cm     torque (average) 680N·cm    it is recommendable to drill
               and
             thrust lines                                                              the bored  hole size as large as
                                                                                       possible.
    CENTER
    DRILLS             After
                        50
                       holes
                      tapping
    Technical
    info                           torque (average) 890N·cm    torque (average) 780N·cm


       404

