


Page 390 - Yamawa_European_Catalogue_YEU21
P. 390
Forming Taps


              SURZ
    Intro


             MP    Multi Purpose Series
    SP        Thread Forming Taps for Stainless Steel, Coated


                                                                       FEATURES
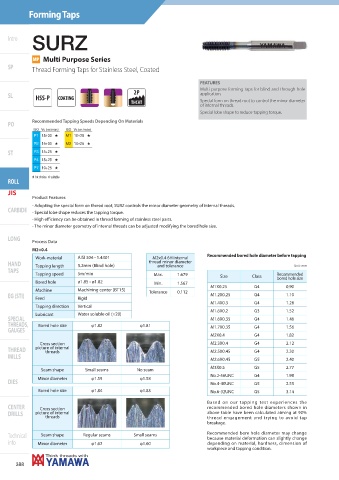
                                                                         Multi purpose forming taps for blind and through hole
                                                2P                     application.
    SL        HSS-P  COATING
                                               THCHT                     Special form on thread root to control the minor diameter
                                                                       of internal threads.
                                                                         Special lobe shape to reduce tapping torque.
            Recommended Tapping Speeds Depending On Materials
    PO
             ISO Vc (m/min)    ISO   Vc (m/min)
                 P1    15÷30     H       M1    10÷25     H
                 P2    15÷30     H       M2    10÷25    H
    ST           P3    15÷25     H
                 P4    15÷25     H
                 P7    10÷25      H
            H 1st choice  I suitable
    ROLL

    JIS                                                                                                 JIS-SURZ
            Product Features
            - Adopting the special form on thread root, SURZ controls the minor diameter geometry of internal threads.
    CARBIDE
            - Special lobe shape reduces the tapping torque.
            - High effi  ciency can be obtained in thread forming of stainless steel parts.
            - The minor diameter geometry of internal threads can be adjusted modifying the bored hole size.

    LONG
            Process Data
            M2×0.4
             Work-material  AISI 304 - 1.4301          M2x0.4 6H internal   Recommended bored hole diameter before tapping
    HAND     Tapping length  5.2mm (Blind hole)      thread minor diameter                              Unit : mm
                                                        and tolerance
    TAPS
             Tapping speed  5m/min                     Max.    1.679          Size        Class   Recommended
             Bored hole     ø1.85 - ø1.82              Min.    1.567                              bored hole size
                                                                           M1X0.25        G4         0.90
             Machine        Machining center (BT15)  Tolerance  0.112
    EG (STI)  Feed          Rigid                                          M1.2X0.25      G4         1.10
                                                                           M1.4X0.3       G4         1.28
             Tapping direction  Vertical
                                                                           M1.6X0.2       G3         1.52
             Lubricant      Water soluble oil (×20)
    SPECIAL                                                                M1.6X0.35      G4         1.46
    THREADS,  Bored hole size    φ1.82            φ1.81                    M1.7X0.35      G4         1.56
    GAUGES
                                                                           M2X0.4         G4         1.82
               Cross section                                               M2.3X0.4       G4         2.12
    THREAD   picture of internal                                           M2.5X0.45      G4         2.30
                 threads
    MILLS
                                                                           M2.6X0.45      G5         2.40
                                                                           M3X0.5         G5         2.77
               Seam shape      Small seams       No seam
                                                                           No.2-56UNC     G4         1.98
              Minor diameter     φ1.59            φ1.58
    DIES                                                                   No.4-40UNC     G5         2.55
              Bored hole size    φ1.84            φ1.83                    No.6-32UNC     G5         3.14

                                                                          Based on our tapping test experiences the
    CENTER     Cross section                                              recommended bored hole diameters shown in
    DRILLS   picture of internal                                          above table have been calculated aiming at 90%
                 threads                                                  thread engagement and trying to avoid tap
                                                                          breakage.

    Technical   Seam shape    Regular seams     Small seams                 Recommended bore hole diameter may change
                                                                          because material deformation can slightly change
    info      Minor diameter     φ1.62            φ1.60                   depending on material, hardness, dimension of
                                                                          workpiece and tapping condition.

       388

